Industrial Packaging Flow and Substrate Compatibility
High-volume carton packaging lines operate under tight schedules where adhesive failure results in pallet shifting, package tampering risks, and automated line stoppages. A standardized setup requires balancing corrugated cardboard materials, environmental temperatures, and roll tensile properties.

Corrugated Material Density
Standard virgin kraft liners present open wood fibers that allow acrylic adhesives to penetrate cleanly. Recycled test liners (RSC) feature shorter, recycled fibers and residual processing chemicals, demanding higher tack adhesives and controlled wipe-down pressure during application.

Dynamic Conveyor Speeds
When cases move rapidly through automated tapers, intermittent shear force pulls at the initial seal tab. The tape film must possess sufficient tensile strength to resist necking down or snapping when sudden acceleration occurs on the conveyor line.

Thermal Working Windows
Warehouses experience seasonal swings from 32 F to 150 F. Water-based emulsion acrylic polymers offer dependable molecular stability across broad thermal margins, preventing both brittle fractures in cold staging areas and adhesive softening in hot transit.
Substrate Engineering: Matching Tape to Carton Grades
Carton surface chemistry dictates adhesive wetting dynamics. Selecting the right tape formulation depends directly on paperboard composition, burst strength ratings, and internal carton content tensions.
| Corrugated Carton Grade | Flute Structure | Substrate Porosity | Recommended BOPP Specification | Primary Failure Mode if Mismatched |
|---|---|---|---|---|
| Virgin Kraft Liner (200# - 275#) | Single Wall (B/C Flute) | High fiber porosity | 45 Micron Standard BOPP | Adhesive starvation due to improper roll wipe-down |
| High-Recycled RSC (100% Post-Consumer) | Single/Double Wall | Dense, short fiber matrix | 50+ Micron High-Tack Acrylic | Edge lifting and flap release under flap spring tension |
| Wax/Poly-Coated Cold Storage Boxes | Double Wall (BC Flute) | Low surface energy, closed pores | High-Coat Weight Acrylic Tape | Total delamination due to poor adhesive wetting |
| Heavy-Duty Bulk Shippers (Triple Wall) | Triple Wall (AAC Flute) | Rigid, high-tensile resistance | 72mm / 3 Inch Heavy-Duty Brown Tape | Center-seam splitting along lengthwise flap deflection |
Application Dynamics: Manual Dispensers vs Automated Case Sealers
Operational bottlenecks emerge when tape physical characteristics do not align with the mechanics of application. Standardizing equipment setups ensures predictable seal longevity.

Manual Hand Dispenser Configurations
Manual sealing relies on pistol-grip hand dispensers utilizing adjustable friction brakes. In high-tempo stations, inconsistent worker pressure leads to poor adhesive contact.
- Brake core must be set to prevent roll over-spin and backlash tangles.
- Wipe-down rubber rollers must exert firm downward thrust along the center seam.
- Standard core dimensions must maintain 3-inch tolerance to eliminate hub wobble.
- Requires BOPP film with high tensile strength to prevent longitudinal split edges during manual cutting.

Automated Case Sealer Integration
Continuous uniform-size or random-size case sealers demand machine-length rolls (990m to 1500m) to minimize line turnover intervals.
- Low and consistent unwind force prevents line-jamming and box skewing during entry.
- Consistent release coating eliminates chatter and static electricity accumulation.
- Spring-loaded wipe-down rollers must provide minimum 30 psi wiping pressure.
- Blade wipe-down arms require precise cut-off cleanly without causing tape edge flagging.
Dimension Sizing: Width, Microns, and Flap Mechanics
Dimensional tape selection balances cost, structural safety factors, and box closure geometry. Applying an undersized tape on high-memory flaps causes immediate line re-work.

48mm (2 Inch) Standard
Suitable for standard RSC cartons up to 40 lbs under normal transit cycles. Fits conventional handheld dispensers and light industrial packaging stations.

72mm (3 Inch) Structural
Recommended for cartons over 40 lbs, wide-gap center seams, and heavy recycled liners. Provides a wider bond area that reduces flap shear stress by 35%.

Film Thickness (Microns)
Film thickness ranges from 38 to 65 microns total. Thicker BOPP backings increase longitudinal tensile resistance and eliminate tear failures during heavy pallet restacking.

Flap End Overlap
Ensure a minimum of 50mm to 75mm (2 to 3 inches) end overlap down the vertical sides of the box to prevent peel initiation from shear vibration in transit.
Browse our full manufacturing line of Packing Tape solutions designed for automated and manual sealing stations.
Unwind Dynamics and High-Speed Dispensing Stability
Unwind tension directly dictates whether tape applies flat without bubbles or undergoes excessive stretching. Film that is stretched over 3% during sealing will exhibit elastic recovery, resulting in curled tape ends and loose box flaps.

Controlled Release Coating
A precision-applied silicone or carbamate release coat ensures the tape roll peels off cleanly without sticking, keeping dispensing smooth and reducing mechanical chatter during high-speed runs.

Static Dissipation in Dry Facilities
Rapid unwind across plastic rollers creates substantial static charge. Static attracts atmospheric corrugated dust onto the freshly exposed adhesive film, degrading carton tack before touch-down.

Acoustic Management in Warehouses
High-volume fulfillment facilities with tens of manual pack stations benefit from low-noise unwind profiles, reducing continuous high-frequency shrieking that causes packing operator fatigue.
Adhesion Quality Control and Destructive Testing
A secure box seal cannot be evaluated by visual inspection alone. Pressure-sensitive acrylic requires mechanical surface engagement to form cross-surface molecular bonds.
Standard Warehouse Verification Methods
Conduct continuous floor audits using empirical testing methods to verify that your packaging tape, line tension, and carton liners are functioning in harmony:
- Fiber Tear Delamination Test: Pull back the tape after 30 seconds of application. If the tape peels cleanly without lifting corrugated paper fibers, adhesive transfer is deficient or wipe-down pressure is low. Complete fiber pull indicates absolute bond security.
- Cross-Hatch Shear Observation: Inspect tape seams along edge overlaps to ensure zero flagging (lifted ends) after transit vibration simulation.
- Creep Resistance under Internal Load: Pack standard cases with test weight and hold at 104 F (40 C) for 24 hours to monitor flap joint displacement along the center line.

Industrial Specification Benchmarks
Ensure incoming raw inventory matches strict technical benchmarks:
180 Peel Adhesion: Greater than 6.0 N/25mm on stainless steel substrates.
Tensile Strength: Minimum 18 lbs/inch width to withstand dynamic drop loads.
Holding Power: Greater than 24 hours under 1kg static shear load at standard factory temperatures.
Manufactured Box Sealing Tape Series
Explore standard, heavy-duty, brown, and custom branded BOPP pressure-sensitive adhesive tapes engineered for continuous carton sealing operations.
-
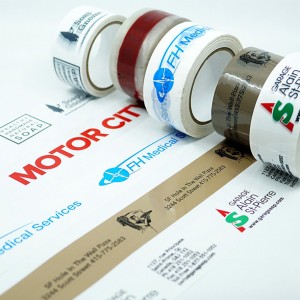
Customized Packing Tape Logo Printed Adhesive Tape Packaging for Shipping
Adhesive: Acrylic Pressure Sensitive Glue
Adhesive Side: Single Sided
Design Printing: Offer Printing
Material: Bopp Film
Feature: Branded Packing Tape
Use for: Carton Sealing
Logo: Custom Logo Printed as Artwrok
-
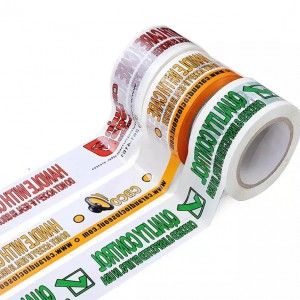
Personalized Custom Tape Packaging Logo Printed Shipping Packing Tape
Size Options: 0.5 Inch (12MM) to 4 Inch (96MM)
Logo Color Choices: White, Black, Blue, Green, Orange, Red, Yellow
Artwork Margin: 1/8 Inch Print Margin
Repeat Spec: Set to a 9.029 Inch Repeat
Function: Advertising, Security, and Anti-Tamper Verification
-
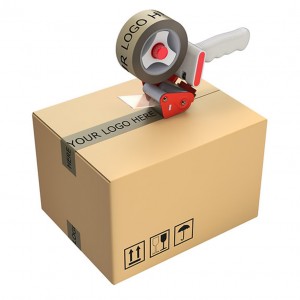
Custom Printed Tape Roll Box Packing Shipping Bopp Tape with Logo
Application: Branding, Promotion, Industrial Sealing
Size: 12 mm - 72 mm Width
Feature: Waterproof and Highly Adhesive
Adhesive Type: Acrylic Based Polymer
Backing: Plastic BOPP Film Base
-
Clear Packing Tape Custom Packaging Carton Sealing Tape
Durability: Thick, Heavy-Grade Acrylic Sealing
Dispenser Fit: Matches Standard Manual Dispensers
Application: Shipping, Moving, Long-Term Storing
Operational Benefit: Fast and Efficient Web Application
-

Heavy Duty Packaging Tape Clear Packing Tape for Shipping Moving Sealing
Grade: Commercial and Industrial Grade
Adhesion: High-Strength BOPP Acrylic Matrix
Thermal Range: Stable in Hot or Cold Temperatures
Purpose: Heavy Packaging Protection Without Splitting
-
Carton Sealing Packaging Tape Heavy Duty Clear Shipping Packing Tape
Tensile Strength: 18 lbs/in High Holding Rating
Temperature Range: 32 F to 150 F Stability
Bond Evolution: Adhesive Matrix Strengthens Over Time
Application: Industrial Corrugated Cardboard Shipping
-
Custom BOPP Packaging Parcel Tape Roll for Packing Box & Moving
Load Capacity: Boxes Weighing up to 80 Pounds
Core Diameter: Standard 3 Inch Industrial Core
Tear Resistance: Engineered Edge-Tear and Split Prevention
Usage: General Warehouse Distribution Packaging
-
Carton Sealing Tape Clear Bopp Packaging Shipping Tape
Grade: Premium Thickness & Toughness
Thermal Profile: Reliable Bonding Across Climates
Cost Performance: Economic Commercial Utility
Integrity: Resists Web Splitting and Snapping
-
Shipping Tape Rolls Packaging Clear Box Packing Tape for Moving
Standard Compliance: Meets Postal and Courier Regulations
Film Toughness: Prevents Transport Abrasion Ruptures
Bond Stability: High Acrylic Holding Strength
Roll Configuration: Standard Core Commercial Packs
-
Carton Packing Tape Box Sealing Clear Adhesive Tape
Adhesive Structure: Polymer Water-Based Acrylic
Appearance: Crystal Clear Lightweight Construction
Sealing Compatibility: Cartons, Envelopes, Bulk Liners
Reliability: Clean Professional Visual Appearance
-
Brown Packaging Tape Carton Box Sealing Parcel Moving Tape
Color: Industrial Kraft Brown / Tan
Compatibility: Paper, Plastic, Metal, Glass Liners
Grade: Heavy-Duty Commercial Sealing Utility
Performance: High Fiber Retention and Clean Holding
-

Packing Tape Brown Bopp Heavy Duty Shipping Packaging Tape
Color Options: Tan, Brown, and Clear Options
Substrate Base: High Tensile BOPP Backing
Durability: Thickened Formulation for Heavy Export Boxes
Integrity: Long-Term Storage and Shipping Stability
Procurement Specifications and Repeat Order Parameters
B2B procurement inconsistency leads to packaging machinery jams and carton failures. Define exact measurable parameters during contract confirmation to prevent production downtime across roll batches.

Total Micron Breakdown
Always specify the split between BOPP base film and acrylic adhesive mass. A 50-micron tape should clearly state 28-micron film plus 22-micron adhesive coat weight to ensure identical shear holding performance across shipments.

Core Caliber and Wall Strength
Tape cores must maintain a true 76mm (3-inch) inner diameter with a rigid 3mm-to-5mm recycled kraft wall. Warped or compressed cores will bind against dispenser mandrels, halting continuous production.

Protective Pallet Packaging
Export rolls must be shrink-towered with interleaved dividers and poly-wrapped to avoid humidity exposure during maritime shipping, preventing edge swelling and telescoping before delivery.
Zhuori Production Capability: Four-Axis PE Cast Film Line
High-standard packaging manufacturing backed by precision equipment, multi-layer co-extrusion technology, and rigorous quality management across over 9,600 square meters of facility area.
Zhuori uses four-station cast film PE stretch film and silage film production lines (1000-4000 mm), combining automated production with stable process control to support consistent film quality and flexible production requirements.
Multi-Layer Co-Extrusion: Flexible material combinations for different film performance requirements.
Automatic Winding & Roll Changing: Four-station winding and 90 automatic roll changing improve roll consistency and production efficiency.
1000-4000 mm Production Width: Supports different film widths, core sizes, and customized specifications.
Stable Production Quality: Standardized production control helps maintain consistent quality across different batches.
About Zhuori (Guangdong) Industry Co., Ltd.
Two decades of packaging materials manufacturing, supplying enterprise-grade stretch wrap films, box sealing packing tape, and high-tensile strapping bands to global brands.

Corporate Timeline & Foundation
1998: Established Guangzhou Nansha YouJan Plastic Co., Ltd.
2002: Established Product Research and Development Center
2008: Established Guangzhou Zhuori Commercial Company
2013: Established Zhuori (Guangdong) Industry Co., Ltd.
Zhuori Group is focused on plastic raw materials as the core of the production plant, professionally manufacturing stretch wrapping film, packing tape, strapping wrap band, and other abundant packaging products. Along with the changes and development of the Offline - Online Internet, Zhuori O2O carries out brand marketing activities with its integrated business model.

Enterprise Partner Operations
At present, the Guangzhou headquarters serves as a hub with nearly 500 team members who have served LG, GREE, TOYOTA, SF Express, Foxconn, Hisense, Panasonic, Midea, Haier, and other global enterprises for nearly 20 years.
With advanced production equipment, good quality products, and rich production experience, the Guangzhou headquarters has become a long-term strategic partner for several global Fortune 500 companies, delivering high standards, refinement, and zero-defect focus from resin formulation to structural verification.
Establish Your Line's Tape Standard Today
Eliminate shipping damage, adhesive popping, and unnecessary roll change frequency. Our packaging engineers assist in configuring tape micron rating, width, roll lengths, and custom printing requirements directly suited to your warehouse throughput.
Contact Information
- +86 18127875878
- sunny@zhuorigroup.com
- No.383, Guangzhu Road, Dagang Town, Nansha District, Guangzhou
Follow Us by


Category
